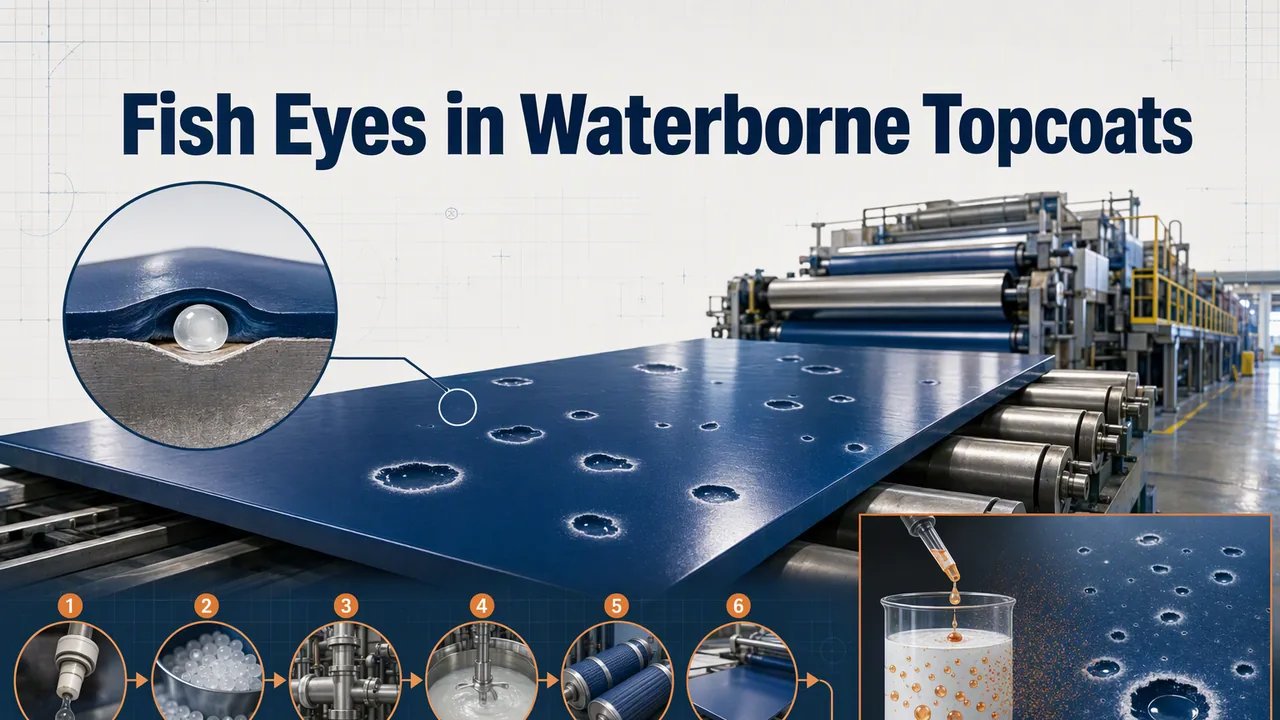
A leather topcoat came off the line with a dozen pinhead craters across one panel, and the first suggestion in the meeting was to add more wetting agent. That is the one move guaranteed to make it worse. A fish eye is a spot where the wet film refuses to sit: something with a lower surface energy than the coating is lying on the panel, and the film pulls away from it. Surface tension wins that argument every time, which is why adding flow agent so often turns twelve craters into sixty.
Fish eyes in waterborne topcoats have six common sources, and only one of them is the coating. Here is how to name yours inside a shift, and what to do about the additive that causes more of them than anything else.
What a fish eye physically is
A crater forms where the coating meets a spot whose surface energy is lower than the coating’s own surface tension. The film cannot wet it, so it retreats, and the liquid piles up at the edge of the retreat to leave the raised ring around a bare centre that everyone recognises. The diameter of that ring is a rough measurement of the contamination. A crater one or two millimetres across came from a visible droplet or a fleck. A field of craters under 0.5 mm usually means an aerosol, a mist or a vapour, and that difference points at different sources.
Two details matter on the shop floor. Waterborne coatings are more sensitive to this than solventborne ones at the same contamination level, because water has a much higher surface tension (about 72 mN/m, against roughly 25 for a typical solvent). And crater rims stay visible after curing even when the crater floor is only a few microns deep, so a defect with no measurable effect on film thickness still reads as a reject at inspection.
Three other defects get called fish eyes and should not be: pinholes from trapped solvent or air, foam craters where a bubble broke before the film levelled, and dewetting on a genuinely oily substrate such as a moulding still carrying release agent. The table separates them.
| What you see | What it is | Confirm it with |
|---|---|---|
| Round bare spot with a raised ring, 1–2 mm | Classic fish eye from a droplet or a fleck of low-energy contamination | Glass-plate spray of the same batch: crater appears there too |
| Dense field of craters below 0.5 mm | Airborne contaminant, mist or vapour, or air-line oil aerosol | Blow test: air only onto a clean glass plate for five seconds |
| Small holes with sharp walls, no ring | Pinholes from trapped solvent or air, not contamination | Check flash-off time, film build and substrate temperature |
| Irregular shallow depressions, often in a band | Foam that broke after application | Look at the tank surface and the return line before the panel |
| Craters only on some parts, worse at edges and corners | Substrate contamination: release agent, oil, or a cleaner that left residue | Water-break test on cleaned and uncleaned parts side by side |
Six sources, in the order we trace them
We run this order because it goes from cheapest to check to most expensive, and it separates the air from the liquid before anybody edits the formula.
- Compressed air. An oil-lubricated compressor with a tired coalescing filter puts fine oil aerosol into every pass. Hold a clean glass plate about 300 mm in front of the gun, trigger air only for five seconds, and read the plate under a light. Streaks or a faint film mean the air is the source, and no additive will fix it.
- The substrate. Mould release, machine oil, hand cream, zinc stearate carried over from a sanding sealer, and silicone polish used on a nearby conveyor are the usual suspects. Test before you coat: a film of clean water that will not hold a continuous sheet for thirty seconds is a surface nothing will wet evenly.
- The coating and its containers. A drum that once held a slip additive, a dip bucket shared with a silicone product, a filter sock reused across mixes. Anything questionable gets a fresh container and fresh filtration before the next trial, not after it.
- Tools, hands and gloves. Nitrile gloves that went through a fabric-softener wash, rags that last touched a silicone lubricant, a spray gun whose air valve was greased with general-purpose grease. Silicone moves between surfaces by touch, so the trace runs backwards through whoever last handled the part.
- The booth and the neighbouring operations. A maintenance crew spraying silicone on a chain, a mould shop next door releasing parts, an open tray of silicone antifoam. Airborne silicone travels. Hang a witness plate in the booth, a bare glass slide left open for a shift, and water-break it at the end.
- The additives you put in on purpose. Last on the list and most often the answer: a slip or anti-scratch additive, an antifoam, or a wetting package topped up one time too many. This is the one place where the fix is subtraction rather than cleaning.
Silicone overdose: when the cure becomes the defect
Slip additives, the silicone-based type in particular, work at concentrations low enough that it is easy to lose track of how much is in the tank. They are supplied as an emulsion of a few percent active material, dosed at a fraction of a percent on total formula. Two habits turn that into a defect.
The first is treating the dose as linear. Slip performance saturates early: past a certain point more additive does not make the surface more slippery, it only increases the free silicone available to crater, to transfer to the next part, and to sit on the surface as a release layer the next coat cannot adhere to. That last effect is the one that hurts, because the symptom arrives late, during recoating or a tape test, which is how a contamination problem becomes a peeling complaint six months later.
The second is topping up a batch that was already dosed. On a two-shift day the night shift sees a defect, adds a little more of whatever the day shift added, and the tank finishes at two or three times the intended loading. If you cannot say what is in the drum you are holding, stop dosing it: dilute a retained sample with water, cast it on a glass plate and look at it dry.
The discipline we recommend is dull and it works. Pre-dilute the additive 1:10 with water, add it in steps of 0.05% on total formula, cast a small panel after each step, and write the running total on the batch card. Never dose a second shift’s worth without a panel from the first shift in hand.
| Additive class | How it goes wrong | First correction |
|---|---|---|
| Silicone slip or anti-scratch | Dose creeps past saturation, or a second shift tops up. Craters appear, and recoat adhesion dies quietly | Stop dosing, cast a panel of the current batch, remake at the last known good loading |
| Antifoam | Dosed beyond the defoamer’s tolerance to knock foam down fast; craters with a sharp centre, sometimes haze | Halve the dose and fix the mechanical aeration instead: pump, return line, high-shear mix |
| Wetting agent | Added to cure craters that something else caused; spreads the defect instead | Identify the contaminant first, before adding a single drop |
Testing each suspect inside one shift
- Blow test the air. If the glass plate stays clean, the air line is exonerated and you can stop maintaining it for now.
- Water-break two panels from the same stack: one as it arrived, one cleaned with the solvent you actually use. The method is standardised as ASTM F22 and gives a go/no-go answer. Partial breaks mean the cleaner is not doing its job.
- Spray the suspect batch on a clean glass plate. Glass carries no oil, no release agent and no grain, so craters there isolate the liquid from the substrate.
- Compare against a retained sample taken before the last top-up, the most useful object in the plant and the one almost nobody keeps.
- Only then change the formula, one variable at a time, with the glass plate as referee. A change you cannot reproduce on glass is a change you have not made.
Scratch resistance without a silicone slip additive
If silicone is the source of the craters, the honest answer is that you may not need it. Mar and scratch resistance can also come from a particle route: a fine wax micro-dispersion that stands slightly proud of the film and takes the abuse instead of the binder. YT-6359 is the additive we ship for that role, at 40 ± 2% solids and pH 7–10, with a wax melting point of 115–130 °C and full water-thinnability at any ratio.
Two numbers decide whether it fits, and both are on its TDS. It is a physical route, so the dose is not a trace amount: 5–10% on total formula is where abrasion resistance shows up in a suitable topcoat. And it is a matte wax paste, so at 5% addition the 60° gloss drops by about 20 units. On a high-gloss clear topcoat that is a non-starter, and we would rather say so than have you find out on a gloss meter. Where the finish is matte or satin to begin with, the matting arrives free with the scratch protection, which is the situation on most leather finishes. One compatibility note from the same sheet: keep C16 alcohol-ester raw materials out of the blend, because the dispersion flocculates with them.
Scratch resistance is also measurable rather than arguable. ISO 1518-1 specifies the constant-loading stylus method, which gives either a pass or fail at a stated load or the minimum load that penetrates the film. Run the old formula and the new one on the same substrate with the same cure, and let the load number settle it.
One distinction worth keeping straight: if your defect is flow rather than dewetting, that is a rheology problem and no surface-tension additive belongs in the answer. Our leveling and sag resistance write-up covers that trade-off, and a nonionic associative leveler such as YT-255D, dosed at 0.5–2.0% of formula, fixes flow without putting silicone near the tank. The wax micro-dispersion route sits in our specialty additive range.
Waterborne topcoat fish eye FAQ
Can I add more wetting agent to cover the fish eyes?
No. A wetting agent lowers the surface tension of the coating, but the contaminant lowers it further at that spot, so the film still pulls away. What changes is the shape of the defect: it often spreads into a wider, shallower crater that reads as haze instead of a ring. Find the contaminant first.
Do I have to strip the whole line once silicone gets in?
Often it is the hose rather than the line. Silicone persists in soft materials, and wiping with cleaning solvent is rarely enough once it has migrated into the hose wall. Replace hoses, filters and any elastomer that touched the silicone batch, flush the hard parts, then recoat a panel. Circulating cleaning solvent through a contaminated line usually just redistributes the silicone.
How do I know the craters came from the coating and not from my panels?
Spray the same batch on a clean glass plate and on a panel from the stack. Glass has no oil, no release agent and no grain, so it separates the variables. Craters on glass point at the coating or the air; craters only on the panels point at the substrate or at how it was cleaned.
If you are chasing cratering on a line and want to know whether the additive in your tank is a slip type or a particle type, ask our application lab with the batch card and one rejected panel. Two photographs and the addition levels are usually enough to name the source.