The order for the switch rarely comes from the adhesive tank. It comes from the permit office, the fire inspector, or a brand audit clause on VOC content, and by the time a slipper or sneaker factory decides to move, the calendar pressure is already on. We have walked enough lines through this conversion to predict the first month: the bond tests fine on the test bench, fails on the third shift, and the team suspects the glue. Nine times out of ten the glue was right and the line was not ready.
What Actually Changes When You Switch
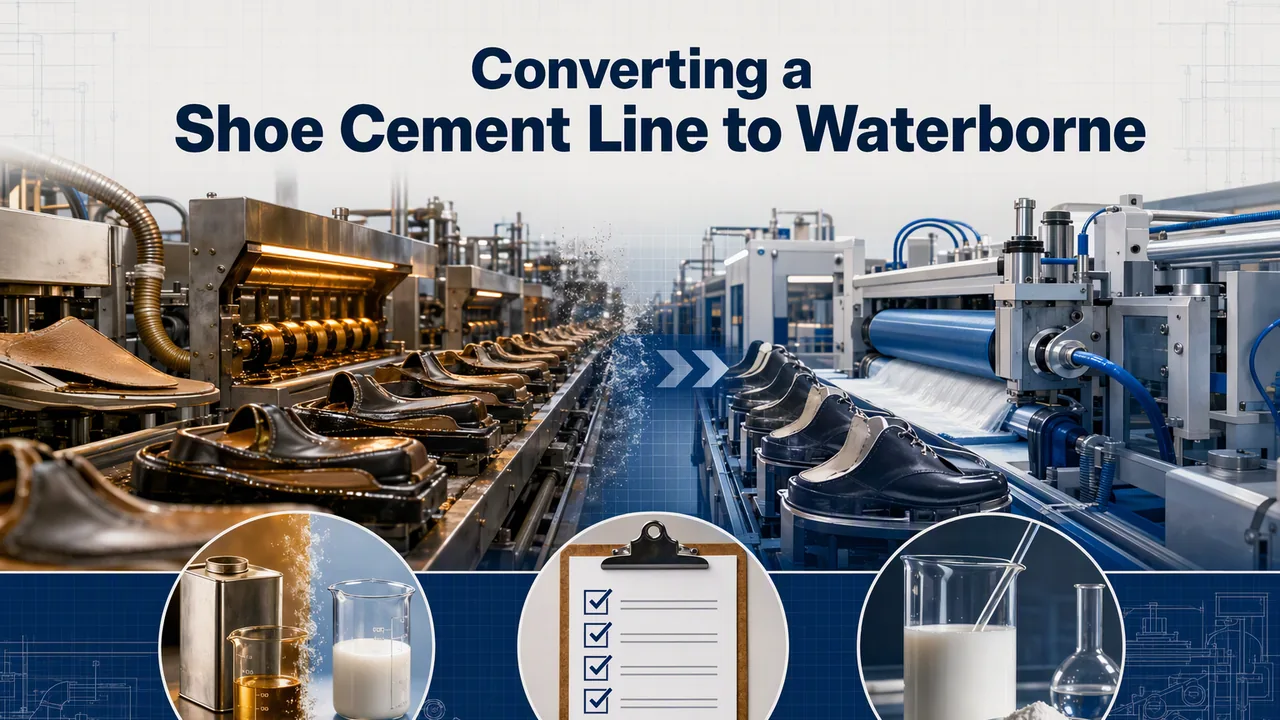
Solvent contact cements, usually polychloroprene, dry fast because the solvent flashes off at room temperature, and they grab on contact. Heat-activated waterborne polyurethane moves the same job into two steps that need energy: water leaves the film slowly and needs airflow and warmth, then the adhesive is triggered at an activation temperature that solvent systems never asked for. That means an oven you did not have before, a humidity window you never had to track, and a cold-weather storage rule, because the drum is an emulsion and freezing is a real event, not a rumor. If your hall runs solvent cement at 25 °C with the doors open, converting to waterborne is a line project, not a product swap.
The Conversion Checklist
- Kill the solvent residue. Empty, dry and re-line tanks, pumps and hoses, or accept that leftover solvent will destabilize the emulsion in hours. Gunk in the tank on day three is almost always this step skipped.
- Dedicate the brushes and rollers. Waterborne PU pulls out of solvent-swollen foam differently, and the first batch of sticky brushes will be blamed on the adhesive.
- Install the activation oven before you schedule the trial, not after. For the fast-drying grades the target substrate temperature is 50–55 °C; for the high-activation grade it is 100–110 °C, which is a bigger box and a bigger bill.
- Rewrite the drying rule: two thin coats beat one heavy coat, and the film must go from milky to clear before pressing. A press operator who cannot see the difference needs five minutes of training, not a new resin.
- Track humidity the way you track oven temperature. Above roughly 75% relative humidity, waterborne flash-off stretches and the whole station slows down; dehumidify or add drying time, but do not thin the adhesive to compensate.
- Prep the substrates honestly. Oily EVA and TPU soles come out of the mold with release agents; wash or plasma-treat them. A bond failure on a mold-oily sole is a molding problem wearing a cement complaint.
- Decide the water-resistance spec up front. If the program needs a wash test, dose 1–5% of a compatible crosslinker; our YT-1102 waterborne curing agent is a polyisocyanate hardener at 19–21% NCO with a 5–6 hour open time, which fits a two-shift day if you mix to the schedule.
- Set the storage and shipping calendar by season. Drums want 5–30 °C. In winter, a container that freezes on the dock is a revive-or-reject decision, and we wrote the test-by-test procedure for exactly that call in the frozen PUD note.
- Budget scrap and a slower first fortnight. Cycle times are longer until the ovens, the habits and the humidity plan are tuned together. The factories that hide this in the trial plan are the ones that abandon the conversion at week three.
Pick the Grade for Your Line
| Grade | Activation | Solids | Best fit on the line |
|---|---|---|---|
| YT-502 | 50–55 °C | 40% | Brush-applied upper cementing, fast activation and crystallization |
| YT-507 | 50–55 °C | 50 ± 2% | Fast-drying spray lines with high scrub resistance demands |
| YT-503 | 100–110 °C | 39 ± 1% | Programs needing anti-blocking and higher heat stability |
All three are anionic waterborne adhesive grades at viscosity under 1,500 mPa·s at 30 °C, so they atomize on existing spray guns and level under a brush without solvent thinning. The full sheets are linked from each product page, and the adhesives application guide covers open time and pressing practice. If your question is really about green tack and activation temperature rather than the switch itself, the earlier heat activation note goes deeper on that trade.
The First 30 Days: Where Trials Fail
The failure list is short and specific. Pressing while the film is still milky, which reads as weak adhesion but is trapped water. Ovens set to air temperature instead of substrate temperature, so the trigger never happens at the bond line. Mixing leftover solvent cement into the waterborne tank to use it up; the two chemistries do not shake hands, and YT-503 is explicitly one you should never blend with adhesives of a different nature. And foaming in the spray tank from a pump that used to run thinner material; keep the pickup pipe submerged and the return line gentle.
What the switch gives back, in fairness: no permit headaches, no solvent storage room, no fire-insurance conversation, and a hall that workers can breathe in. The regulatory pressure that pushed you here is not going away, and the EPA's VOC guidance is the same conversation in Washington that your brand is having in its audit checklist.
Shoe Cement Conversion FAQ
Is the cycle time really longer than solvent cement?
Yes, by minutes per station, until tuned. Water needs heat and airflow that solvent never asked for. A line with a proper oven and a humidity plan closes most of the gap within a month of running, but do not let anyone promise you solvent speed on the first trial.
Will waterborne PU hold on oily TPU soles?
Not on mold-oily surfaces, and no cement will. Wash or abrade, and for stubborn TPU run a primer pass. We would rather you spend thirty seconds on the sole than a week blaming the adhesive.
Can we run solvent and waterborne on the same line?
You can, with separate tanks, separate brushes and a cleaning ritual at the changeover, and most factories end up doing it during the transition year. Keep the solvent station downstream of the waterborne one so overspray never travels the wrong way.
If your trial is stalling on one station, send us the sole material, the oven reading at the bond line and a photo of the failure surface. The fix is usually one of the nine checkboxes, not a new resin.